Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
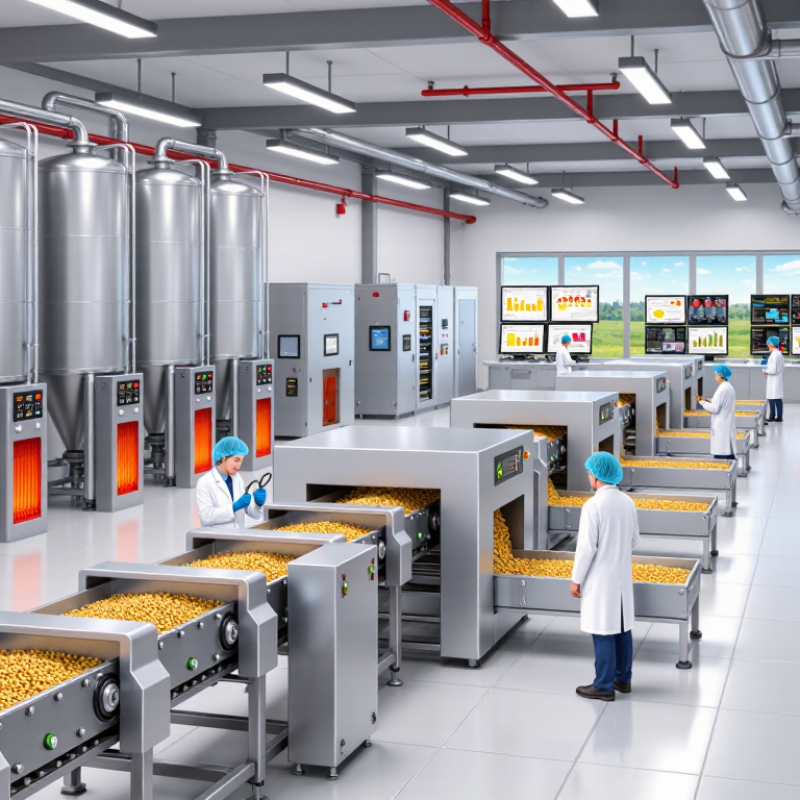
Improving Oilseed Preparation in 2026 will require more than faster machines or higher production targets. It will require disciplined control from receiving to pressing, extraction, and storage. In practical terms, teams must inspect seed moisture, foreign material, temperature, and microbial risk before processing begins. A simple moisture imbalance can reduce dehulling efficiency and increase energy consumption.
Professor Fereidoon Shahidi, a leading authority on edible oils and lipid science, has stated, “Oxidation is the major cause of deterioration in fats and oils.” His observation remains highly relevant for modern Oilseed Preparation. Clean equipment, controlled heating, short residence times, and oxygen-limited storage can protect oil quality. Operators should also track peroxide value, free fatty acids, moisture, and residual solvent where applicable. Small changes matter.
Digital monitoring will become more practical in 2026. Sensors can identify temperature spikes near the flaking rolls, while automated sampling can reveal quality drift before a full batch is affected. Yet technology is not a substitute for experience. A well-calibrated sensor can still support a poor decision. This is where documented procedures, trained personnel, and independent laboratory checks strengthen reliability.
The industry also needs honest reflection. Not every factory can justify expensive automation immediately. Some facilities may gain more from repairing worn screens, improving ventilation, or cleaning storage bins. The best strategy depends on seed variety, scale, climate, and final product requirements. Effective Oilseed Preparation should therefore combine measurable data with practical judgment, protecting yield, food safety, and long-term equipment performance.
How to Improve Oilseed Preparation in 2026?
Assessing oilseed quality is the foundation of effective preparation. A clean appearance alone proves little. Check moisture, foreign materials, insect damage, broken kernels, and free fatty acid levels. Use representative samples from different parts of each delivery. One handful can mislead.
Moisture strongly influences storage and processing. Excess moisture may encourage mold, heating, and poor separation. Very dry seeds can create dust and increase breakage. Measure moisture with calibrated equipment, then confirm unusual results through laboratory testing. I have seen operators trust a single reading too quickly. That decision later caused uneven pressing.
The preparation method should match the seed condition and final product. Cleaning suits lots with stones or plant residue. Dehulling may improve meal quality when hulls are thick. Cracking helps release oil, while controlled conditioning can improve extraction efficiency. Cold pressing may suit carefully selected, high-quality seeds. Mechanical pressing is not always the best answer. Monitor temperature, residence time, and particle size during each stage. Keep records for every batch, including rejected material and corrective actions. Small details matter. Review the process when oil yield drops, even if the equipment appears normal. Sometimes the problem begins with sampling, not machinery.
Effective oilseed preparation begins before pressing. Cleaning and sorting remove stones, dust, metal fragments, damaged seeds, and unwanted plant material. In practical plant work, small impurities can create large problems. Dust may overload filters. Stones can damage equipment. Uneven moisture can also change seed flow and extraction performance.
Use calibrated screens, aspiration, magnets, and optical sorting where suitable. Screens should match seed size and shape. Airflow must remove light debris without carrying away valuable kernels. Magnets help capture ferrous fragments before crushing. Optical systems can identify discolored or damaged seeds, but they require clean lenses and regular checks. Operators should inspect samples during each production shift. Equipment settings are never truly “set and forget.”
Tips: Keep a simple inspection log. Sample incoming lots consistently. Record moisture and impurity levels. Check rejected material for good seeds. Clean sensors daily. Avoid changing airflow too quickly. I once saw excessive aspiration remove useful kernels with the chaff. The lesson was uncomfortable but clear: cleaner is not always better. Small losses deserve measurement, not guesswork.
How to Improve Oilseed Preparation in 2026?
Drying should begin with measurement, not habit. Incoming seed can vary sharply across a single truckload. Check moisture at the top, middle, and bottom of each load. Record temperature beside every reading. Warm seed may appear drier than it is. That mistake can invite mold during storage. FAO reports that 14% of food is lost between harvest and retail, often through weak post-harvest handling (The State of Food and Agriculture 2019). Better moisture control can reduce part of this preventable loss.
Use gradual drying when possible. Excessive heat can darken seed, damage proteins, and reduce oil quality. Set airflow according to seed type, initial moisture, and ambient humidity. Soybeans, rapeseed, and sunflower seed do not share one safe target. Confirm limits with validated storage tables, such as those published in USDA grain-storage guidance. A calibrated meter matters. So does cleaning it. Small residue can distort readings.
Conditioning needs equal attention. After drying, allow seed to rest until moisture redistributes through the kernel. Test again before crushing. Shortcuts are tempting. They are also expensive. Operators should compare moisture readings with press performance, extraction yield, and cake temperature. This creates useful plant-specific evidence. A perfect curve is unrealistic. Weather changes, equipment ages, and sampling is never flawless. Review the process monthly, then adjust fan speed, residence time, and conditioning temperature carefully. The best 2026 systems will treat moisture as a moving variable, not a fixed number.
How to Improve Oilseed Preparation in 2026?
Improving Dehulling, Size Reduction, and Flaking Efficiency
Efficient oilseed preparation starts with consistent raw material checks. Measure moisture, foreign matter, seed size, and hull condition before processing. These details influence dehulling performance and reduce unnecessary wear on screens and rolls. A practical target is even hull removal without damaging too many kernels. Excessive cracking can increase fines and complicate later separation. Small adjustments matter.
Dehulling works best when equipment settings match seed variety and moisture. Monitor hull separation visually and verify it with regular samples. For size reduction, avoid treating every seed batch the same way. Gap settings, rotor speed, and feed rate should respond to kernel hardness. Flaking also requires balance. Thin flakes improve heat transfer, but overly thin flakes may create dust and block airflow. Operators should check flake thickness across the full roll width, not only at the center.
Tips: Clean magnets, screens, and feeding areas frequently. Record moisture and particle-size results each shift. Keep spare screens available during seasonal changes. Watch for rising motor load; it may signal poor conditioning or uneven feeding. Do not chase maximum throughput too early. A slower, stable line often gives better recovery. Some settings will need revision after real production data appears. That is normal.
| Process Area | Key Performance Dimension | Recommended 2026 Target | Typical Improvement Opportunity | Verification Method |
|---|---|---|---|---|
| Cleaning | Foreign material removal | At least 98% removal of readily separable stones, stems, dust, and metal particles | Improve screening, aspiration, magnet inspection, and separator adjustment before dehulling | Incoming and cleaned-seed mass balance; periodic laboratory inspection |
| Moisture Conditioning | Seed moisture before dehulling | Generally 9–12% for soybeans; optimize separately for sunflower, rapeseed, and other oilseeds | Use controlled tempering to reduce hull adherence and prevent excessive kernel breakage | Moisture test at intake, after tempering, and immediately before dehulling |
| Dehulling | Hull removal efficiency | Approximately 85–95% hull removal, depending on seed type and final product specification | Balance rotor speed, clearance, feed rate, and seed moisture instead of maximizing mechanical intensity | Measure hull content in dehulled kernels and residual hull in the kernel stream |
| Dehulling | Kernel recovery | Keep whole and large kernel recovery above 90% where product specifications allow | Reduce over-conditioning, excessive rotor speed, and narrow clearances that create splits and fines | Screen dehulled material by size and calculate whole-kernel recovery by mass |
| Aspiration | Hull separation and air balance | Maintain stable air velocity and minimize kernel carryover in the hull stream | Install differential-pressure monitoring and adjust air volume as feed rate changes | Analyze hull-stream samples for kernel loss at least once per shift |
| Size Reduction | Particle-size distribution before flaking | At least 90% of particles within the selected preparation range; avoid excessive powder formation | Use a controlled crack-and-size-reduction step rather than excessive grinding | Use sieve analysis and track the percentage of fines below the process limit |
| Size Reduction | Fines generation | Keep fines below 5–8%, unless the downstream extraction process requires a different specification | Control roll gap, differential speed, screen condition, and feed uniformity | Sieve test at startup, after changeovers, and during throughput changes |
| Flaking | Flake thickness | Approximately 0.25–0.40 mm for many solvent-extraction preparations | Maintain consistent roll gap, roll parallelism, feed distribution, and seed temperature | Measure thickness at multiple points across the roll width using a calibrated gauge |
| Flaking | Flake integrity | Minimize powder and unflattened kernels; target a stable appearance across the full production run | Prevent uneven feed, worn rolls, excessive moisture variation, and unstable roll pressure | Visual inspection plus sieve analysis of fines and unflattened material |
| Energy Management | Specific energy consumption | Establish a site baseline in kWh per metric ton and reduce it by 5–10% without lowering product quality | Avoid over-processing, monitor motor load, and schedule roll and screen maintenance | Record electricity use and throughput continuously; compare by seed type and moisture |
| Process Stability | Throughput consistency | Keep hourly throughput within ±5% of the approved operating setpoint | Use automatic feed-rate control and alarm limits for moisture, motor load, pressure, and temperature | Review production data by hour and investigate deviations using statistical process control |
| Quality Control | Oil recovery potential | Improve extraction performance by maintaining uniform flakes and limiting fines, rather than relying only on higher mechanical intensity | Correlate flake thickness, residual oil, fines, and extraction yield in a daily process dashboard | Track residual oil in meal and oil yield against preparation quality results |
| Maintenance | Critical wear and alignment | Inspect rolls, screens, bearings, magnets, aspiration ducts, and sensors according to condition-based limits | Replace worn contact surfaces before they cause thickness variation, excess fines, or higher energy use | Use vibration, temperature, motor-load, and product-quality trends for preventive decisions |
How to Improve Oilseed Preparation in 2026?
Oilseed preparation needs tighter control from intake to extraction. The OECD-FAO Agricultural Outlook 2024-2033 projects oilseed production to reach about 695 million tonnes by 2033. More volume increases quality pressure.
At receiving, measure moisture, temperature, foreign material, and insect damage for every lot. Keep a traceable sample. Test high-risk materials for aflatoxins and other mycotoxins under Codex limits and local rules. Moisture alone is not enough. Water activity can reveal hidden storage risk. Dry seeds quickly, but avoid excessive heat that may damage proteins and natural antioxidants. Clean equipment between lots. Small residues can contaminate a larger flow.
Processing performance also needs measurable targets. Monitor dehulling efficiency, flake thickness, conditioning temperature, oil recovery, meal protein, and residual oil. The U.S. Department of Agriculture’s Oilseeds: World Markets and Trade reports show how global supply, crushing, and trade changes affect processing decisions. A stable line should connect these figures with plant data, not rely on habit.
Nutritional checks deserve equal attention. Track fatty acid profiles, tocopherols, peroxide value, and protein solubility. A higher extraction rate may reduce nutritional quality. That trade-off is easy to overlook. Pilot trials may still fail because laboratory results ignore seasonal variation. Review rejected lots, not only successful ones. Experience becomes useful when it is recorded, challenged, and corrected.
Monitoring safety, nutritional quality, and processing performance across major oilseed types.
The chart combines typical whole-seed oil and protein composition values with practical moisture-conditioning targets. The safety reference uses the European Union maximum level of 5 µg/kg for aflatoxin B1 in applicable food categories; regulatory limits can vary by product and market. Moisture, oil, and protein values are representative reference values for raw seeds rather than company-specific data.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift