Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
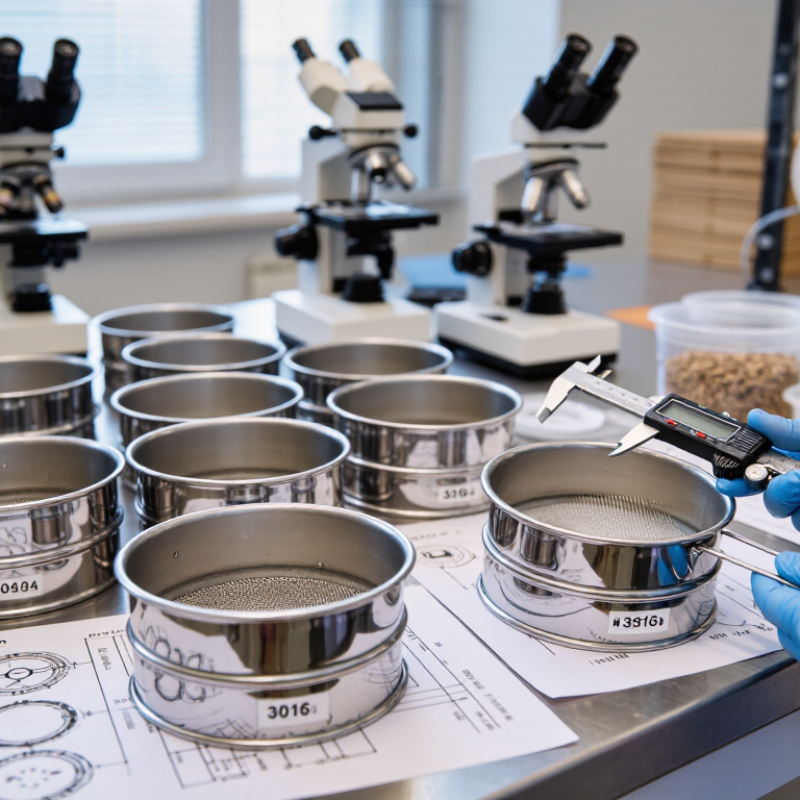
Choosing Fine Mesh Tamis for global sourcing requires more than comparing mesh counts and unit prices. A tamis may look identical in a supplier’s photograph, yet differ in wire diameter, aperture tolerance, frame stiffness, and cleaning performance. These details affect particle separation, product yield, and production downtime. Small differences matter.
Industry data supports a more disciplined approach. The World Bank’s Logistics Performance Index 2023 emphasizes customs efficiency, shipment reliability, and supply-chain traceability as major sourcing factors. UNCTAD’s Review of Maritime Transport 2024 also highlights continuing exposure to route disruption, freight uncertainty, and longer transit planning. For food and pharmaceutical applications, buyers should connect commercial decisions with recognized technical controls, including ISO 3310-1 for test sieves and ASTM E11 requirements for woven wire testing sieves. These standards do not replace supplier audits. They create a common technical language.
Price is only one variable. A low-cost Fine Mesh Tamis can become expensive after repeated deformation, blocked apertures, or inconsistent batch results. Request dimensional drawings, material certificates, mesh inspection records, surface-finish details, and sample testing before approval. Confirm whether stainless steel means 304, 316, or another grade. That distinction is easy to overlook. It should not be.
Supplier capability also deserves direct verification. Review production photographs, calibration practices, export experience, packaging protection, and corrective-action records. Independent inspection can expose problems that polished samples hide. Still, no sourcing method is perfect. Specifications may be incomplete, and laboratory results may not represent continuous production. A resilient 2026 strategy therefore combines standards, physical samples, transparent documentation, and realistic landed-cost analysis.
2026 How to Choose Fine Mesh Tamis for Global Sourcing
A fine mesh tamis is a precision screening tool made from woven wire, perforated metal, or synthetic mesh. It separates particles by controlled aperture size. “Fine” has no universal cutoff. In practice, buyers often specify openings below 1 millimeter, but the correct size depends on the material and process.
Fine mesh tamis support flour grading, pharmaceutical powder screening, chemical filtration, mineral classification, and liquid pre-filtration. They can remove lumps, protect pumps, and improve batch consistency. A 2024 industrial filtration market report estimated the global market above US$30 billion in 2023, with growth near 5% annually through 2030. This demand reflects tighter process control across manufacturing. ASTM E11-24 and ISO 3310-1 provide useful references for mesh dimensions and test sieves. However, a mesh number alone can mislead. Aperture tolerance, wire diameter, tension, and cleaning conditions also affect performance.
Tips: Request the aperture in micrometers, not only mesh count. Confirm the material’s temperature, chemical, and wear resistance. Ask for inspection records and a sample test. Do not assume a finer tamis always improves output. It may increase pressure loss, clogging, and maintenance. Global sourcing also needs clear edge dimensions, frame design, certificates, and packaging requirements. Specifications are often incomplete. That is where costly mistakes begin.
| Mesh Designation | Nominal Aperture | Typical Wire Diameter | Approx. Open Area | Fine Mesh Tamis Definition | Typical Industrial Applications | Recommended Material | Key Sourcing Considerations |
|---|---|---|---|---|---|---|---|
| Fine Mesh Tamis Selection Guide by Aperture Size | |||||||
| 20 mesh | 850 µm 0.850 mm | 0.35–0.45 mm | Approximately 45–52% | A fine screening tamis used to separate coarse powders, granules, and small particles. | Mineral powders, ceramic granules, agricultural products, food ingredients, and coarse pharmaceutical excipients. | 304 stainless steel for general service; 316 stainless steel for corrosive or hygienic environments. | Check particle size distribution, required throughput, and whether the product tends to clog the openings. |
| 30 mesh | 600 µm 0.600 mm | 0.25–0.32 mm | Approximately 48–55% | A medium-fine tamis for classifying powders and granules below the coarse screening range. | Flour and starch processing, chemical powders, pigments, feed materials, and general laboratory particle classification. | 304 stainless steel; electroformed nickel may be considered where very consistent openings are required. | Confirm whether the specification is based on ISO, ASTM, or another national standard because mesh naming can vary. |
| 40 mesh | 425 µm 0.425 mm | 0.20–0.28 mm | Approximately 45–52% | A fine screening tamis commonly used for controlled separation of small granules and agglomerated powders. | Food powders, pharmaceutical granules, chemical intermediates, additive manufacturing powders, and laboratory testing. | 316L stainless steel is preferred for hygienic, cleanable, and corrosion-sensitive applications. | Request aperture tolerance, wire diameter, frame flatness, and surface-finish information for quality control. |
| 60 mesh | 250 µm 0.250 mm | 0.14–0.20 mm | Approximately 42–50% | A fine mesh tamis for separating smaller powder particles while maintaining practical screening capacity. | Pharmaceutical powders, fine chemicals, powdered coatings, food additives, toner-related materials, and research laboratories. | 316L stainless steel for product-contact applications; 304 stainless steel for less demanding dry service. | Evaluate screening method, vibration intensity, cleaning procedure, and the risk of blinding from damp or cohesive powders. |
| 80 mesh | 180 µm 0.180 mm | 0.12–0.16 mm | Approximately 40–48% | A fine tamis designed for relatively narrow particle classification and removal of small oversize particles. | Pharmaceutical excipients, fine ceramic powders, powdered pigments, specialty chemicals, and precision laboratory analysis. | 316L stainless steel or nickel mesh where high dimensional consistency is important. | Ask for calibrated test-sieve certification, effective screening area, and inspection records for the mesh cloth. |
| 100 mesh | 150 µm 0.150 mm | 0.10–0.14 mm | Approximately 38–46% | A very fine screening tamis for powder classification at the lower end of conventional laboratory sieve testing. | Fine pharmaceutical ingredients, mineral fillers, ceramic materials, food powders, pigments, and quality-control laboratories. | 316L stainless steel is generally suitable for corrosion resistance, cleanability, and repeated use. | Define the required test method, sample mass, sieving time, and acceptable mass-retained tolerance before purchasing. |
| 140 mesh | 106 µm 0.106 mm | 0.07–0.10 mm | Approximately 35–44% | An ultra-fine tamis used when the process requires separation of particles close to one-tenth of a millimeter. | Fine chemicals, pharmaceutical powders, metal powders, advanced ceramics, mineral processing, and specialized research work. | 316L stainless steel; precision nickel mesh can be used for demanding dimensional applications. | Prioritize uniform aperture distribution, low mesh distortion, careful handling, and a validated anti-blinding method. |
| 200 mesh | 75 µm 0.075 mm | 0.05–0.075 mm | Approximately 32–40% | An ultra-fine mesh tamis for high-resolution particle classification and removal of very small oversize fractions. | Pharmaceutical and chemical research, fine mineral powders, pigments, battery-material research, and specialty ceramics. | 316L stainless steel, nickel, or other application-specific precision mesh. | Confirm that the selected sieve standard covers the requested aperture and that the screening equipment can prevent mesh blockage. |
| Material, Construction, and Compliance Factors for Global Sourcing | |||||||
| 304 stainless steel | Available across fine mesh ranges | Selected according to aperture and strength requirements | Determined by aperture-to-wire ratio | General-purpose stainless-steel tamis material with good corrosion resistance and mechanical strength. | Dry food ingredients, general chemicals, minerals, ceramics, laboratory screening, and non-aggressive process streams. | Use when the product and cleaning chemicals are not highly corrosive. | Specify material grade, mesh standard, weld quality, frame material, and whether the mesh is tensioned or bonded. |
| 316L stainless steel | Available across fine mesh ranges | Selected according to aperture and strength requirements | Determined by aperture-to-wire ratio | Low-carbon stainless steel commonly selected for improved corrosion resistance and hygienic product-contact service. | Pharmaceuticals, biotechnology, food processing, salt-containing products, marine-related service, and corrosive chemicals. | Suitable where frequent washdown, sanitation, or exposure to chlorides and process chemicals is expected. | Request material certificates, surface-finish data, passivation details, and cleaning compatibility information. |
| Electroformed or precision nickel mesh | Often used below approximately 150 µm | Precisely controlled, application-specific | Often higher uniformity than woven mesh at very small apertures | A precision mesh made by electroforming, typically selected for consistent micro-openings and repeatable geometry. | Precision filtration, micro-powder classification, electronics-related materials, laboratory research, and specialized manufacturing. | Use when aperture uniformity is more important than maximum mechanical flexibility. | Verify nickel compatibility with the product, aperture measurement method, thickness, and allowable dimensional deviation. |
| Woven wire mesh | Commonly specified by mesh count and aperture | Depends on weave, aperture, and required strength | Usually lower as wire diameter increases | The most common tamis construction, made by interlacing warp and weft wires in a plain or other controlled weave. | Laboratory test sieves, industrial screening, food and pharmaceutical processing, chemical production, and mineral classification. | Choose plain weave for many standard fine-screening applications; confirm the weave and mesh direction where relevant. | Specify nominal aperture rather than mesh count alone, because identical mesh counts can have different openings. |
| Perforated plate | Typically larger than fine woven-mesh apertures | Plate thickness is application-specific | Depends on hole shape, pitch, and plate thickness | A rigid screening surface with punched or drilled openings, generally used where impact resistance is more important than ultra-fine separation. | Heavy-duty scalping, aggregate processing, abrasive materials, and high-load screening stages. | Use for coarse separation or protective screening rather than the finest powder classification. | Check open-area percentage, hole tolerance, plate flatness, wear resistance, and compatibility with the screening machine. |
| Practical Purchasing Checklist | |||||||
| Aperture specification | State in µm or mm | Include tolerance | Relates directly to separation cut size | The nominal opening between adjacent wires and the primary dimension used to define screening performance. | All industries using particle classification, contamination removal, or quality-control testing. | Use the applicable ISO, ASTM, or national standard for the required test method. | Do not purchase solely by “mesh count”; request the nominal aperture and permitted deviation. |
| Frame and diameter | Common laboratory frames include 200 mm and 300 mm diameters | Frame depth varies by equipment and sample volume | Screening area affects capacity | The supporting ring or frame that holds the mesh and enables stacking or machine installation. | Laboratory testing, pharmaceutical production, food processing, chemical plants, and mechanical screening systems. | Stainless steel frames are preferred for cleanability and long service life. | Confirm outside diameter, inside diameter, frame depth, stack compatibility, and machine interface dimensions. |
| Cleaning and hygiene | Application-specific | Must not damage fine wires | Clean mesh preserves effective open area | The procedures and design features used to remove retained material without deforming the mesh. | Food, pharmaceutical, biotechnology, cosmetics, and high-purity chemical applications. | 316L stainless steel with smooth, crevice-minimized construction is commonly selected. | Define ultrasonic cleaning, spray washing, dry-cleaning, sanitation chemicals, and maximum allowable temperature. |
| Certification and inspection | Calibration may include aperture measurement and conformity records | Traceability should match the purchase order | Verification supports repeatable results | Documentation confirming mesh aperture, material, dimensions, and conformity with the selected standard. | Regulated manufacturing, contract laboratories, pharmaceutical quality control, and international procurement. | Request a certificate of conformity and, where necessary, an individual calibration certificate. | Agree in advance on inspection sampling, measurement method, labeling, packaging, and document language. |
| Packaging and logistics | Protective packaging is essential for fine mesh | Avoid compression and impact | Damage can alter aperture and open area | Packaging designed to prevent bending, contamination, corrosion, and deformation during international transport. | All global sourcing projects involving laboratory sieves, replacement mesh, or assembled screening units. | Use clean, dry, corrosion-protective packaging suitable for the transport route and storage period. | Specify individual protection, moisture control, shock protection, carton dimensions, and export labeling requirements. |
Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift