Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
Choosing an Mcb Assembly Robot is not simply a matter of comparing cycle times. It means matching automation to your products, people, and production constraints. A line assembling miniature circuit breakers may handle several models, delicate springs, and small terminals. Each detail affects feeding, gripping, and inspection. Miss one, and the robot may run quickly but still create bottlenecks.
Robotics pioneer Joseph Engelberger once said, “I can’t define a robot, but I know one when I see one.” For factory buyers, seeing is not enough. Ask suppliers to demonstrate your actual components, changeover process, and target production rate. Check assembly accuracy, error detection, guarding, maintenance access, and how the system handles rejects. Request evidence from comparable installations, not only a polished showroom cycle.
The right Mcb Assembly Robot should fit today’s workload and leave room for realistic product changes. Review the full cell, including feeders, fixtures, testing equipment, and operator tasks. Confirm who provides training, spare parts, and troubleshooting support. A technically impressive machine can still disappoint. That part deserves reflection.
This guide will help you compare robot types, production needs, integration requirements, and supplier claims. It will also point out questions to ask before investing. No checklist replaces a factory trial. Your components may behave differently at speed, and a small feeding issue can stop an entire line. Start with measurable requirements, then validate them under production-like conditions.
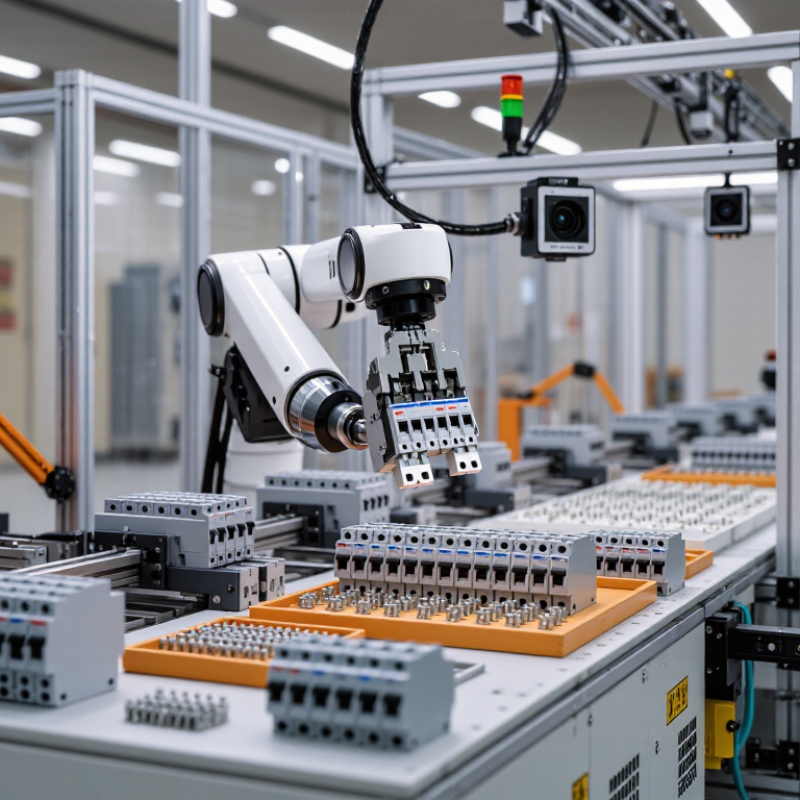
Before comparing an MCB assembly robot, map the work it must perform. List each breaker rating, pole configuration, and component variant. Record the current output per shift, target cycle time, changeover frequency, and acceptable defect rate. Include manual inspection and rework; these often disappear from early calculations. Small details matter, like how operators load contact parts or clear a jammed feeder.
Set goals against measured production, not optimistic estimates.
The International Federation of Robotics’ World Robotics 2024 report recorded 541,302 industrial robot installations worldwide in 2023, reflecting broad automation investment, but it does not establish the right capacity for your line.
Your own takt time and demand forecast should guide sizing. Define traceability needs, including which assembly steps require recorded test results or serial-level data. Specify space, utilities, operator access, and links to upstream component feeding and downstream testing.
Be practical. A faster station can simply move the bottleneck. Leave room for uncertainty: product mix changes, and supplier parts may vary. A pilot run with real components can expose missed handling problems before final specifications are fixed.
Keep the assumptions visible, especially expected uptime and planned maintenance hours.
How to Choose an MCB Assembly Robot for Your Factory?
Choosing an MCB assembly robot starts with the actual tasks: placing springs, fitting contacts, or fastening small components. SCARA robots suit fast, planar movements, while six-axis models handle angled operations and more complex access. Cartesian robots can work well when motion follows fixed, straight paths. Match the robot type to your station layout, part presentation, and required cycle time. More axes are not always better.
Tips: Check repeatability, not just advertised accuracy. Compare the robot’s performance with component tolerances and fixture variation. Test the gripper on real parts; a tiny spring can slip or rotate during transfer. Vision may help with inconsistent part positions, but it cannot fix poor feeding. Short trials reveal useful problems.
Look at the full assembly cell, including feeders, tooling, sensors, and operator access. A robot may meet its motion specification yet miss the line’s takt time after pauses and part changes. Ask suppliers for a representative demonstration using your components and production sequence. Record placement errors, recovery time, and changeover steps. No trial is perfect, and early results can be misleading, so leave room for adjustment before committing to a final configuration.
How to Choose an MCB Assembly Robot for Your Factory?
Check Compatibility with Components, Tooling, and Factory Systems
Start by listing the MCB models the robot must assemble, including pole counts, housing dimensions, terminal positions, and accessory options. Even small differences in enclosure shape can affect gripping or component alignment. Ask the integrator to test representative parts from actual production batches, not only ideal samples. A fit that works once may not stay reliable across normal component variation.
Check whether the tooling suits each assembly step. Grippers need to hold housings without marking them, while screwdrivers must reach terminals and apply controlled torque. Feeders should present parts in a consistent orientation. Quick-change tooling can help with product changes, but it adds setup checks. Small details matter. Record changeover time during a practical trial; estimates can be optimistic.
The robot also needs to work with your factory systems. Confirm compatibility with existing PLCs, sensors, safety interlocks, and production data requirements. Check available floor space, power, air supply, and how operators will access the cell for routine adjustments. A spreadsheet can miss awkward cable routes or a hard-to-reach reset button. Run a pilot cycle using real parts and normal staffing, then review jams, inspection results, and recovery time before approving the final layout.
When choosing an MCB assembly robot, compare verified output with your factory’s actual demand. A quoted cycle time may exclude feeder jams, model changeovers, inspection, and operator loading. Ask for a sustained production rate using your own breaker components. Watch a full shift if possible. Short demonstrations can hide small delays that add up.
Safety depends on the whole cell, not just the robot. Check guarding, access doors, emergency stops, and safe restart behavior. Confirm how the machine handles a misfed terminal or a rejected unit. These details affect both operator protection and production flow. Review the layout with the people who will run and maintain it. They often notice awkward reach points that a drawing misses.
Calculate total ownership costs across the expected service life. Include installation, tooling, spare feeders, training, energy, maintenance, and downtime. Compare these costs with good units produced, not theoretical cycles. Ask how quickly common wear parts can be replaced, and whether troubleshooting requires specialist support. Estimates are still estimates; product mix and staffing can change the result. Keep that uncertainty visible in the budget.
When choosing an MCB assembly robot, look beyond its quoted cycle time. Ask suppliers for layouts, component compatibility details, and references from factories with similar product ranges. A machine that handles one breaker size well may struggle with another terminal design or a slightly uneven parts tray. Ask for evidence. Request a sample run using your actual components, not demonstration parts.
Agree on factory acceptance tests before purchase. Check assembly accuracy, cycle consistency, reject handling, and recovery after a feeder jam. Record results across a sustained run, then inspect finished breakers for misplaced parts or loose connections. Test the awkward parts. A brief demonstration can hide problems that appear after several hours. No test catches every shop-floor surprise, so leave room for practical adjustments.
Installation needs careful coordination. Confirm floor space, power, air supply, guarding, and access for maintenance before delivery. Have operators and technicians join commissioning, and make sure training includes fault recovery, changeovers, and routine checks. Ask what support is available after handover: response times, spare-part availability, software updates, and remote troubleshooting. Put those details in writing. A low purchase price can feel less attractive when production stops and no replacement sensor is on hand. It is also worth asking how the supplier documents changes; this detail is easy to overlook, and sometimes teams do overlook it.
Use this scorecard to compare supplier proposals for a miniature circuit breaker (MCB) assembly line. Assign each criterion a score from 0 to 5: 0 = no evidence, 3 = meets the documented requirement, and 5 = exceeds it with verifiable evidence. Calculate the weighted result as score ÷ 5 × weight.
| Evaluation dimension | Weight | What to verify | Evidence to request | Score (0–5) | Weighted result |
|---|---|---|---|---|---|
| Product and process fit | 15% | Confirm the proposed stations cover the actual assembly sequence, components, variants, and required operations. Identify manual tasks and process assumptions. | Process flow, station layout, cycle-time breakdown, product-family matrix, and a list of customer-supplied parts or tooling. | _____ | _____ / 15 |
| Capacity and line balance | 10% | Compare the demonstrated cycle time and planned operating pattern with the factory’s required output. Check whether loading, inspection, changeover, and planned downtime are included in the capacity assumptions. | Cycle-time study, station-by-station capacity assumptions, line-balance chart, and a sample production run using representative parts. | _____ | _____ / 10 |
| Flexibility and changeover | 8% | Check compatibility with the MCB variants, component tolerances, and future product changes in scope. Review how recipes, fixtures, and tooling are selected and controlled. | Variant and tooling matrix, changeover procedure, recipe-management demonstration, and a changeover trial between representative models. | _____ | _____ / 8 |
| Assembly quality controls | 12% | Verify how the machine detects missing, misoriented, or incorrectly assembled parts and how process parameters are monitored. Agree on defect definitions and acceptance limits before testing. | Control plan, inspection method descriptions, error-proofing list, sample defect challenge results, and agreed quality acceptance criteria. | _____ | _____ / 12 |
| Factory and acceptance testing | 10% | Define Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT) in advance. Use agreed samples, operating conditions, test duration, data collection, and pass/fail criteria. | Draft FAT/SAT protocols, test-piece requirements, measurement methods, issue log, and a sample completed test report. | _____ | _____ / 10 |
| Traceability and data access | 8% | Establish what production and quality data are recorded, how rejects and alarms are logged, and how records can be exported. Confirm interfaces and data ownership. | Sample production record, data-point list, export demonstration, interface specification, and data-retention and access terms. | _____ | _____ / 8 |
| Machine safety and compliance | 10% | Review risk assessment, guarding, access points, emergency stops, safety-related controls, electrical documentation, and applicable local legal requirements. Confirm responsibilities for conformity assessment. | Risk assessment, safety-function documentation, electrical schematics, applicable standards and compliance plan, and safety validation records where available. | _____ | _____ / 10 |
| Factory integration | 7% | Check footprint, utilities, material flow, upstream and downstream interfaces, controls connectivity, and site constraints. Clarify which party supplies each interface and connection. | Layout and utility requirements, interface list, signal or network specification, and a site-readiness checklist. | _____ | _____ / 7 |
| Installation and commissioning | 7% | Agree on installation scope, schedule, required site resources, commissioning activities, and the process for resolving open issues before handover. | Installation plan, responsibility matrix, commissioning checklist, handover criteria, and a defined escalation route for schedule or technical issues. | _____ | _____ / 7 |
| Training and documentation | 4% | Confirm that operators, maintenance staff, and engineers receive role-appropriate training and usable documentation in the required language. | Training agenda, operating and maintenance manuals, spare-parts list, troubleshooting guide, and electrical and mechanical drawings. | _____ | _____ / 4 |
| Ongoing service and spare parts | 5% | Review service channels, support hours, response and escalation commitments, remote-support arrangements, spare-parts availability, and warranty terms. | Written service-level terms, warranty scope, recommended critical-spares list, parts lead-time information, and support contact process. | _____ | _____ / 5 |
| Total cost and commercial clarity | 4% | Compare the full project scope, including tooling, installation, training, software or licenses, spares, and stated exclusions. Consider expected maintenance and operating costs over the planned service life. | Itemized quotation, scope and exclusions, payment milestones, warranty details, and a lifecycle-cost estimate with stated assumptions. | _____ | _____ / 4 |
| Total weighted score | Compare suppliers only after confirming that the proposed scope and test assumptions are equivalent. | Maximum possible result: 100 points. | — | _____ / 100 | |
Decision gate: Before purchase approval, resolve safety and compliance responsibilities, document measurable FAT/SAT acceptance criteria, confirm product and process compatibility, and agree on installation scope and post-installation support.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift