Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES
OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
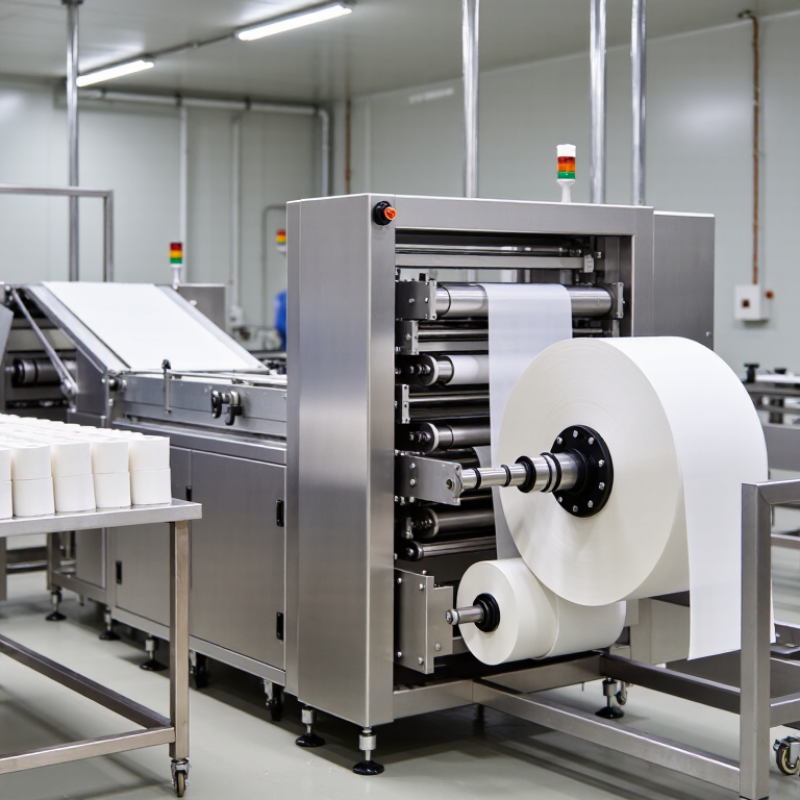
Choosing a Facial Tissue Cutting Machine is not a small equipment decision. The right model can help a converting line produce neat, consistent packs while reducing avoidable trim waste and downtime. Yet a machine that looks impressive in a brochure may not fit your actual tissue grade, roll width, or daily output target.
This guide presents seven practical tips for comparing options. Start with product specifications: cutting accuracy, supported tissue dimensions, operating speed, and changeover time. Then consider blade type, guarding, controls, spare-part access, and the supplier’s commissioning and maintenance support. Ask for a demonstration using material close to your own. Watch the cut edges, listen for unusual vibration, and check how quickly operators can clear a routine jam. Small details matter.
There is no single best machine for every plant. A high-speed unit may be a poor match for a small team or an inconsistent upstream feed. Likewise, the cheapest quotation can hide costs in tooling, service, or setup. I would treat supplier claims as starting points, not proof; request measurable test results and clarify what they include. Even these checks cannot predict every production issue. A careful comparison, based on real operating needs, gives buyers a firmer basis for choosing a Facial Tissue Cutting Machine that can perform reliably over time.
Set Tissue Inputs Using ISO 12625 Grammage and Strength-Test Data
A cutter performs best when its settings reflect the actual parent roll, not a catalog average. Record each lot’s grammage in grams per square metre using ISO 12625-3, then check tensile strength under ISO 12625-4. These measurements help explain why two rolls with identical dimensions may cut differently. One may stretch or tear more easily at the blade.
Use your test report to compare grammage and tensile results across several samples, not just one strip. ISO 187 specifies testing conditions of 23 ± 1°C and 50 ± 2% relative humidity; consistent conditioning makes comparisons more meaningful. Small differences matter. For example, a trial roll measuring 16 g/m² with lower tensile strength may need a gentler feed or sharper blade than a stronger roll of similar grammage. Treat that as a starting point, not a universal setting.
Log the roll ID, test values, blade condition, feed speed, and edge quality after each run. If the cut shows feathering, check strength variation before changing several machine settings at once. I have seen teams trust a single average too quickly; it can hide weak spots across the web. Retest, adjust one variable, and keep the imperfect result in the record. That record often proves more useful than memory. Sources: ISO 12625-3, ISO 12625-4, and ISO 187.
Compare grammage with machine-direction (MD) and cross-direction (CD) tensile strength before setting cutting and handling conditions. Grammage is determined using ISO 12625-6; tensile properties are determined using ISO 12625-4.
These illustrative sample values show how measured tissue properties can be organized for input selection; they are not ISO limits or machine-setting specifications. Test the actual tissue lot and confirm settings with production trials.
Match the machine’s cutting width and sheet length to the tissue as packed, not just to the jumbo roll. Confirm the open-sheet dimensions, fold pattern, ply count, and sheets per pack with a physical sample. For example, a 200 mm square sheet folded once has a different finished footprint from a 200 × 210 mm sheet. Small differences matter. A pack that is too wide may bulge at the seal; one cut too short can leave awkward gaps between sheets.
Ask suppliers to clarify which dimension their specifications call “cutting width” and which means cross-cut length. Terms are not always used consistently. Check usable web width after edge trim, blade tolerance, and how the machine handles changes between pack sizes. A short trial using your own tissue can reveal frayed edges, uneven stacks, or sheets that pull apart poorly. These details are easy to miss on a quotation.
The broader market is growing, which makes format flexibility useful. Grand View Research estimated the global tissue paper market at USD 87.6 billion in 2022 and projected a 6.4% compound annual growth rate from 2023 to 2030. That figure covers tissue products beyond facial tissue, so it is context, not a facial-pack forecast. Still, it supports checking whether one machine can handle your current pack and a realistic future size. Be cautious: chasing every possible format can add setup complexity you may not need.
The dimensions below are practical examples of facial tissue formats, not fixed industry standards. Confirm finished-sheet dimensions, folding pattern, stack height, and pack measurements against your product specification and machine supplier’s drawings.
| Tip | Pack format | Example open-sheet size | Cutting-width and sheet-length check | What to verify before purchase |
|---|---|---|---|---|
| 1. Start with the actual sheet size | Standard rectangular pocket or box tissue | About 200 × 200 mm | Check that the machine can consistently produce the required cut dimension for the folded stack, rather than relying only on the nominal open-sheet size. | Measure samples after unfolding; record both dimensions and the permitted tolerance. |
| 2. Match the machine range to rectangular sheets | Rectangular box tissue | About 200 × 210 mm | Confirm the usable cutting-width range covers the folded-log configuration for both the shorter and longer sheet dimensions. | Request a dimensional layout showing the direction of feed, fold, and cut for your product. |
| 3. Account for square sheets | Square-sheet box tissue | About 210 × 210 mm | Check that the cutter and guides can handle the required folded-stack dimensions without forcing an unsuitable orientation. | Test the intended fold pattern; equal open-sheet sides do not necessarily mean equal folded-stack dimensions. |
| 4. Include compact pocket packs in the specification | Pocket tissue, commonly around 7–10 sheets per pack | Often about 180–200 × 200 mm; confirm the product design | Verify the shorter cut length and narrow folded stack can be controlled accurately, especially at higher line speeds. | Run samples at the smallest planned format and inspect edge squareness and pack fit. |
| 5. Check larger sheets and pack dimensions | Large-format or premium box tissue | About 210 × 230 mm, depending on the product | Make sure the maximum cutting width and machine clearance accommodate the folded log and intended cut length. | Compare the finished stack with the carton’s internal dimensions, allowing for compression and packaging clearance. |
| 6. Check sheet count and stack height | Box packs commonly specified by count, such as 80, 100, or 200 sheets | Use the specified open-sheet size for the chosen pack | Cut length sets the footprint; sheet count, ply, and basis weight affect stack height and should not be treated as cutting-width adjustments. | Confirm the cutter can handle the target stack dimensions and the downstream packer’s infeed limits. |
| 7. Allow for changeovers and tolerances | A product range with multiple sheet sizes or pack formats | For example, 200 × 200 mm and 200 × 210 mm | Choose a machine whose adjustment range covers every specified cut length and width, with repeatable settings after changeover. | Ask for the supported size range, adjustment method, changeover time, and achievable cutting tolerance in writing. |
Note: Open-sheet dimensions and machine cutting dimensions are not always measured in the same direction. Confirm the machine’s reference points and product orientation before finalizing specifications.
When comparing a facial tissue cutting machine, treat its rated sheets per minute as a reference, not a guaranteed shift result. Ask how the figure was measured: tissue ply, sheet length, stack height, and whether stops were included. A rating of 6,000 sheets per minute equals 360,000 sheets per hour on paper. Actual output can fall when operators reload parent rolls, clear jams, or change formats. Small pauses add up. Compare the rating with your required output using the same units and time period.
Estimate demand from finished packs per hour, sheets per pack, and planned operating hours. Then account for roll changes, blade checks, cleaning, and downstream limits. If orders require 300,000 good sheets per hour, a machine that can only sustain that exact rate leaves no room for interruptions. That is tight. Request a production trial using your tissue grade and target dimensions, and record usable sheets rather than total cuts. Check whether speed stays steady as stacks form and transfer. I would question any estimate based only on a short demonstration; real shifts are messier. Compare trial results with peak demand, and allow practical headroom without buying capacity your line cannot use.
Blade precision shows up in the tissue edge, not just on a machine specification sheet.
Check several stacks for ragged corners, uneven sheets, and dust near the cut. Small marks matter. Ask how blade alignment is checked and how often sharpening or replacement is needed. A sharp cut can still drift after extended running, so inspect samples from both startup and steady production.
Changeover time should include more than the minutes spent swapping a blade or format part. Record the time from the last acceptable pack to the first stable pack in the new setup. Include adjustment, test cuts, and discarded sheets. Keep the operator and material consistent during comparisons; otherwise, the numbers are hard to trust.
That number can mislead. A fast changeover is not useful if the machine needs repeated fine-tuning afterward.
Track material waste by cause, such as startup sheets, edge trim, jams, and rejected packs. Use the same denominator for each machine, such as kilograms processed, and compare similar tissue grades. A neat spreadsheet can hide inconsistent counting.
I would review actual waste bins alongside production records, even if that takes extra time.
Not always obvious. Look for recurring patterns, like more offcuts after a format change or dusty edges when speed rises.
A facial tissue cutting machine combines fast blades, moving web rolls, and pinch points in a compact space. Review its risk assessment against ISO 12100:2010, which guides hazard identification and risk reduction. Look closely at blade access during threading, cleaning, and jam removal. Guards should prevent reach-in, while interlocks should stop hazardous motion when opened. Test emergency stops from the operator’s normal working positions. Small gaps matter.
The International Labour Organization’s 2023 safety report estimates
2.93 million work-related deaths and 395 million non-fatal work injuries worldwide each year.
These figures are broad, not specific to tissue converting, but they show why safety checks deserve attention. For electrical design, IEC 60204-1:2016+A1:2021 covers machinery electrical equipment. Inspect the cabinet for clear labels, secure wiring, suitable grounding, and protection against unexpected restart after power loss.
Ask for documented test results, not only a checklist. Also observe a real stop-and-restart cycle; paperwork can miss awkward controls or confusing indicators. I would still question any design that depends on operators remembering a hidden reset step.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift