Taking Custom Design to New Levels
PROUD TO BE PART OF THE BRIN FAMILY OF COMPANIES

OTHER BRIN LOCATIONS
Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN
Choosing the 2026 Best Chipboard Slotting Machine requires more than comparing prices or catalog photographs. Global buyers need equipment that performs consistently across board thicknesses, production speeds, and workshop conditions. A dependable machine should create clean, accurate slots without excessive chipping, vibration, or material waste. Small details matter.
This guide examines practical features, including spindle stability, adjustable slot width, feeding accuracy, dust extraction, safety guarding, and control-system usability. It also considers maintenance access, spare-parts availability, operator training, and supplier communication. These factors often decide whether a machine supports long-term production or becomes an expensive obstacle. A sample test using real chipboard sheets can reveal problems that specifications hide.
The evaluation reflects common workshop experience, not only manufacturer claims. Buyers should inspect cutting results, measure slot tolerances, and request videos from comparable applications. Energy consumption and noise levels deserve attention too. They are easy to overlook. No single model suits every factory, and this article may not capture every regional requirement or future technology change. That limitation matters. Import duties, electrical standards, floor space, and local service capacity can alter the final decision. Reliable purchasing therefore depends on evidence, transparent documentation, and careful comparison. The strongest choice balances precision, productivity, safety, serviceability, and total ownership cost for the buyer’s actual operation.
A chipboard slotting machine is industrial equipment designed to cut precise grooves, channels, or slots into chipboard panels. These openings support folding, joining, nesting, and component assembly. In packaging, slots help form rigid cartons and protective inserts. In furniture production, they guide shelves, backs, and connecting panels.
Its purpose is controlled material removal. A feeding table moves each panel toward rotating cutters, while guides keep the board aligned. Adjustable depth settings determine how far each cutter enters the surface. Some machines also provide multiple slot patterns, dust extraction, and digital control. These functions reduce repeated measuring and help operators maintain consistent dimensions across large batches.
Reliable operation depends on more than cutting speed. Operators should check board thickness, moisture, cutter sharpness, and feed pressure before production. A small alignment error can create loose joints or visible gaps. Safety guards and emergency stops require regular inspection. In practice, no machine performs perfectly under every condition. Thin chipboard may chip at the edges, especially with worn tooling. Test cuts remain useful, even when production settings seem familiar. Global buyers should compare working width, slot depth range, power requirements, maintenance access, and documentation before purchase.
A chipboard slotting machine converts flat sheets into accurately folded carton blanks. The process begins with a stack feeder. Vacuum cups or friction belts separate each sheet and move it toward the infeed table. Side guides correct drift before the sheet reaches the scoring and slotting section. Small errors matter here.
Rotating knives then remove narrow sections of board, creating slots for folding flaps and locking tabs. Creasing rules press fold lines without cutting through the sheet. Operators adjust knife depth, spacing, and pressure according to board thickness. A practical setup often requires test sheets, because moisture and fiber direction can change the result. Waste strips move into a collection area, while sensors check feeding and sheet position. The finished blank exits for folding, gluing, or manual inspection.
Smithers’ 2024 folding-carton market analysis projects global demand to grow at roughly 3% annually through 2029. That growth increases pressure for stable output and lower material waste. PMMI’s 2024 packaging workforce report also highlights continuing skills shortages in manufacturing. Simple controls help, but they do not replace trained setup judgment. Experienced operators watch for crushed edges, incomplete slots, and uneven creases. These defects may appear minor, yet they can stop automatic carton forming later. Machine buyers should compare usable speed, changeover time, dust control, and inspection capability—not only the advertised strokes per minute.
This chart shows the standard operating sequence of a chipboard slotting machine. The numbers indicate process order, not machine speed or production capacity.
Smithers reports that the global packaging market reached about USD 1.17 trillion in 2023 and may approach USD 1.38 trillion by 2028. This growth increases pressure on chipboard converters to improve accuracy, uptime, and material flexibility. When comparing slotting machines, check the board thickness range first. A practical model should process common chipboard grades without crushing edges or causing uneven grooves.
Slot width and depth matter more than headline speed. For retail cartons, ask for stated tolerances, not general claims. A 0.1 mm difference can affect folding quality. Confirm maximum sheet size, minimum sheet size, feed stability, and dust-control design. PMMI’s 2024 packaging machinery industry reporting identifies labor availability and automation as major investment concerns. Automatic setup, recipe storage, and tool-less adjustments can reduce changeover time. Measure the real result.
Fast is not always better. Test continuous feeding with warped sheets. Review servo response, motor load, extraction volume, and noise levels. Safety systems should align with ISO 12100, ISO 13849-1, and IEC 60204-1. I would also examine remote diagnostics, spare-part lead times, and local technician coverage. Some buyers overlook these details. That mistake becomes expensive during peak orders. Vendor performance data should include factory acceptance tests, sample cartons, energy consumption, and documented service records.
2026 Best Chipboard Slotting Machine for Global Buyers
For export projects, a chipboard slotting machine must fit real production conditions, not just a catalog image. Stable slot depth, clean cutting edges, and adjustable guides help maintain consistent box dimensions. Servo-driven positioning can reduce setup errors during repeated orders. Quick tool changes also matter when packaging designs change frequently. A clear control panel supports operators with different experience levels. Ask for sample testing before purchase. It reveals issues that specifications may hide.
Tips: Check the machine’s voltage, frequency, and plug configuration before shipment. Confirm the working width, slot depth range, blade material, and dust-collection connection. Request videos of actual cutting tests, not only factory demonstrations. Keep spare blades and essential sensors in the export package. These small details can prevent long delays after installation.
Reliable export equipment also needs complete documentation. Installation guides, wiring diagrams, maintenance schedules, and safety instructions should be available in clear English. Remote technical support is useful, but it cannot replace practical training. A short online session may not solve every adjustment problem. Buyers should evaluate packaging strength, moisture protection, loading methods, and replacement-part availability. Global projects often face uncertain delivery conditions. The machine may perform well, yet poor packing can still create expensive trouble. Clear acceptance criteria and recorded test results make cooperation more dependable.
| Evaluation Dimension | Recommended Specification for Global Projects | Typical Reference Range or Requirement | Why It Matters to Buyers | Pre-Shipment Verification |
|---|---|---|---|---|
| Machine Type | Automatic or semi-automatic rotary slotting machine for corrugated or chipboard packaging production | Select according to board format, production volume, and required automation level | The machine configuration must match the buyer’s actual packaging workflow | Confirm machine layout, process sequence, and sample production test |
| Maximum Sheet Size | Choose a working width and length that exceed the largest planned sheet size by a practical operating margin | Common industrial formats include approximately 1,200–2,500 mm sheet width and 2,000–4,500 mm sheet length | Adequate capacity reduces trimming, repositioning, and production restrictions | Run the buyer’s largest approved sheet and verify feeding stability |
| Minimum Sheet Size | Specify a minimum format suitable for small cartons and short-run orders | Often approximately 350–600 mm in the smallest feed dimension, depending on the machine design | A suitable minimum format improves flexibility for mixed product portfolios | Test small-format samples for feeding, registration, and ejection |
| Board Thickness | Adjustable pressure and tooling for the board grades used in the export project | Typical compatible thickness is about 1.5–10 mm; confirm the actual range with the tooling design | Correct pressure protects the board surface and prevents crushed edges | Process thin, medium, and thick samples and inspect slot quality |
| Slotting Depth | Tooling with adjustable slotting depth and replaceable knives | Common production settings are approximately 20–100 mm, subject to board structure and product design | Adjustability supports different carton depths and folding requirements | Measure slot depth at multiple positions on the same sheet |
| Production Speed | Variable-speed drive with stable feeding at the buyer’s target output | Typical rated speeds range from approximately 60–180 sheets per minute, depending on sheet size and configuration | Rated speed should be evaluated together with actual usable output and setup time | Conduct a continuous production run and record output, stoppages, and rejects |
| Registration Accuracy | Servo or precision mechanical adjustment with repeatable positioning | A practical target for industrial packaging work is approximately ±1.0–2.0 mm, depending on material and process | Accurate slot alignment improves folding, gluing, and final carton appearance | Measure slot position against the approved drawing using calibrated tools |
| Changeover System | Handwheel, digital, or servo-assisted adjustments with clear scales and stored settings | Tool-free or quick-lock changeover is preferred for frequent product changes | Shorter setup time reduces waste and improves small-batch profitability | Time a complete changeover between two approved product formats |
| Control System | Industrial PLC, touchscreen HMI, fault display, recipe storage, and multilingual operating interface | English interface should be available; additional languages may be specified in the purchase contract | Clear controls simplify operator training and troubleshooting in overseas plants | Check language settings, alarm messages, recipe recall, and backup procedures |
| Electrical Compatibility | Factory-configured electrical system with suitable motor protection and documented wiring | Common industrial supplies include 380–415 V, three-phase, 50 Hz; local requirements must be confirmed before ordering | Correct electrical configuration prevents commissioning delays and unsafe modifications | Verify voltage, frequency, phase, current, terminal markings, and wiring diagrams |
| Installed Power | Select motor capacity based on sheet format, tooling load, speed, and auxiliary equipment | Many medium-duty configurations fall within approximately 8–30 kW installed power | Power demand affects plant capacity planning, operating cost, and export-site installation | Record nameplate data and verify running current under normal load |
| Safety Features | Emergency-stop circuits, guarded rotating parts, interlocked access doors, overload protection, and warning labels | Safety design should be documented and adapted to the destination market’s regulations | Safety controls reduce operator risk and support workplace compliance | Test every emergency stop, guard switch, alarm, and restart-prevention function |
| Dust Management | Enclosed cutting area or prepared extraction ports with accessible cleaning points | Provide extraction airflow requirements in the technical documentation where applicable | Effective dust control protects product quality, equipment life, and the working environment | Inspect dust outlets and operate the machine with the planned extraction system |
| Tooling and Spare Parts | Replaceable slotting knives, scoring tools, bearings, belts, sensors, and electrical consumables | Include an initial spare-parts kit and a complete parts list with technical drawings | Local availability of wear parts reduces downtime after installation | Check part quantities, dimensions, material specifications, and identification labels |
| Quality Inspection | Documented factory acceptance test using buyer-approved board, drawings, and production parameters | Inspect slot position, depth, edge condition, throughput, noise, alarms, and reject rate | A repeatable acceptance procedure creates objective evidence before shipment | Approve signed test records, sample cartons, photographs, and measurement results |
| Noise and Work Environment | Low-vibration structure, balanced rotating components, and clearly stated operating noise data | Where required by local rules, verify workplace noise against the applicable occupational limit | A controlled work environment improves operator comfort and factory compliance | Measure sound level at the operator position during normal operation |
| Documentation Package | English user manual, electrical diagrams, pneumatic diagrams if applicable, maintenance schedule, spare-parts list, and test report | Documents should identify machine model, serial number, revision date, and applicable technical parameters | Complete documentation supports customs clearance, installation, and operator training | Review documents digitally before dispatch and include a printed set with the machine |
| Export Packing | Moisture protection, shock-resistant blocking, corrosion protection for metal surfaces, and clearly marked lifting points | Packing should be suitable for multimodal transport and the expected storage duration | Proper packing reduces transport damage and simplifies handling at the destination | Inspect packing photos, package dimensions, gross weight, center of gravity, and lifting marks |
| Installation and Training | Remote commissioning support or on-site service, operator training, maintenance instruction, and troubleshooting guidance | Define training hours, travel requirements, language, scope, and acceptance criteria in advance | Structured commissioning reduces ramp-up time and improves first-month productivity | Complete installation checklist and confirm trained operators can run approved samples |
| Warranty and Service | Written warranty, remote technical support, response-time commitment, and spare-parts supply process | Commercial terms commonly define a 12-month warranty from installation or shipment; contract wording must be confirmed | Clear service terms protect production continuity after international delivery | Confirm warranty exclusions, service channels, escalation contacts, and replacement-part lead times |
| Buyer Selection Priority | Prioritize board compatibility, repeatable accuracy, safety, maintainability, electrical compatibility, and total cost of ownership | Compare at least capacity, usable speed, energy demand, tooling cost, training, warranty, and logistics requirements | The most suitable machine is not always the one with the highest rated speed | Use a weighted technical-commercial evaluation sheet before issuing the purchase order |
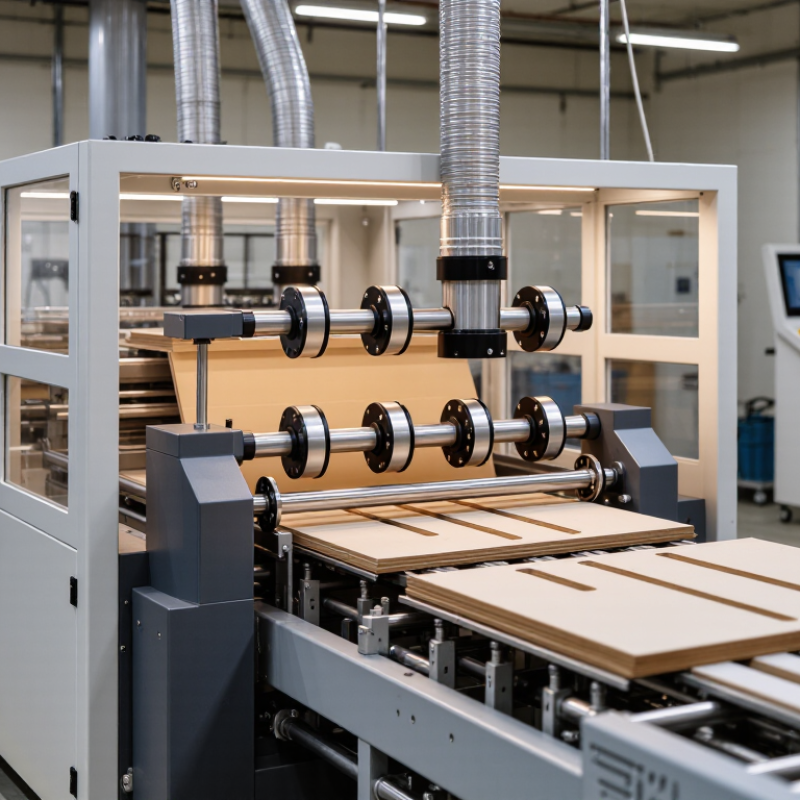
A chipboard slotting machine needs a controlled installation, not simply a level floor and electrical connection. Check foundation strength, ventilation, guarding clearance, and material flow before positioning the machine. IEC 60204-1 supports careful electrical verification, while ISO 12100 requires risk assessment during design and operation. I still see buyers overlook dust collection. That mistake becomes expensive.
Maintenance should follow measured wear, not a convenient calendar. Inspect slotting knives, belts, bearings, sensors, and emergency stops each shift. Record vibration, temperature, rejected sheets, and adjustment changes. The U.S. Bureau of Labor Statistics reported 2.4 nonfatal workplace injuries per 100 full-time private-industry workers in 2023. OSHA’s FY2023 Top 10 report also kept machine guarding among its leading violations. These figures support disciplined inspection, not informal shortcuts.
Buyer selection should compare usable output, board thickness range, changeover time, noise, dust control, and spare-part availability. Request acceptance-test records using your actual chipboard. Ask for training hours and remote troubleshooting limits. A high speed rating can hide slow setup. That happens. Verify electrical compatibility, operator access, guarding interlocks, and documentation in your language. Maintenance access matters more than glossy specifications. Choose measurable reliability over impressive claims.
Taking Custom Design to New Levels

Brin Glass Company | Minneapolis, MN
St. Germain’s Glass | Duluth, MN
Heartland Glass | Waite Park, MN

Fabricator
Inside Sales and Client Support Manager
Glass Handler – 1st Shift